For a concentrated sulfuric acid pump handling 80% to 98% acid at moderate temperature, a centrifugal pump in gray cast iron or carbon steel is the standard and most economical choice. The acid itself forms a protective iron sulfate film on the metal. Below 80%, above 60 °C, or wherever the concentration can drop, that film breaks down, and a fluoroplastic-lined pump is the safer choice. This guide gives the limits for each option, shows how to size the motor for an acid that weighs 1.84 times as much as water, and lists what to put in the purchase order.
| Acid condition | Pump to consider | Limits |
|---|---|---|
| 80–98%, 25–50 °C | GBW pump in gray cast iron (HT200/HT250) | Concentration 80–98%, temperature 25–50 °C |
| 80–98%, 25–60 °C | GBW pump in WCB carbon steel | Concentration 80–98%, temperature 25–60 °C |
| Below 80%, or a concentration that varies | IHF fluoroplastic-lined centrifugal pump or CQB-F lined magnetic drive pump | Up to 80 °C, no thermal shock, motor sized for SG 1.84; magnetic drive must never run dry |
| Transfer from a tank or sump | Fluoroplastic submerged pump | 6–50 m³/h, 12–28 m head |
| Small or intermittent transfer | Air-operated diaphragm pump, PTFE version | Check PP and PVDF versions against the concentration |
| Oleum (fuming acid, above 100%) | Not cast iron; ask us about carbon steel | See the red lines below |
Concentrated sulfuric acid (sulphuric acid in British English) is a strong oxidizer. When it touches iron or carbon steel, it forms a thin layer of iron sulfate that separates the metal from the acid and slows further attack. That film is what protects a GBW pump. Its gray iron is ordinary HT200 or HT250 without large alloy additions; the protection comes from the acid, not from the alloy.
The film only survives in strong acid. Below 80% it dissolves, and the corrosion rate rises sharply. The range from 65% to 80% is the worst of all for iron. The concentration therefore has to stay above 80% in every operating state, including startup, shutdown, flushing and upsets. For the longest life, keep it at the strong end of the range.
Water is the usual cause of trouble. A water flush, a leaking cooler or moist air drawn into a tank can dilute the acid inside the pump. Dilution also releases a great deal of heat, so acid must always be added to water, never water to acid. Do not leave water or weak acid standing in an iron pump: drain it fully, and follow your site procedure for any flush.
High-silicon cast iron (STSi15R) is a different material. It resists sulfuric acid across the whole concentration range, but it is expensive, very brittle and hard to machine. It is used in other pump types, not in GBW.
The iron sulfate film is soft, and fast flow wears it away. Industry guidance for carbon steel piping in concentrated acid limits the flow velocity to about 0.9 m/s. Inside a pump the speeds are far higher: at 2,900 rpm, the tip of a GBW impeller between 100 mm and 250 mm in diameter moves at roughly 15 to 38 m/s.
GBW pumps are designed for this, but they are not suited to very high-velocity duties, and anything that adds turbulence shortens their life:
- Gas bubbles and cavitation, which scour the film. Keep a clear margin between NPSH available and NPSH required.
- Running far from the best efficiency point, especially when throttled close to shutoff.
- Solids in the acid, which abrade the film.
For the hydraulic side of selection, see our guide on how to select a centrifugal pump.
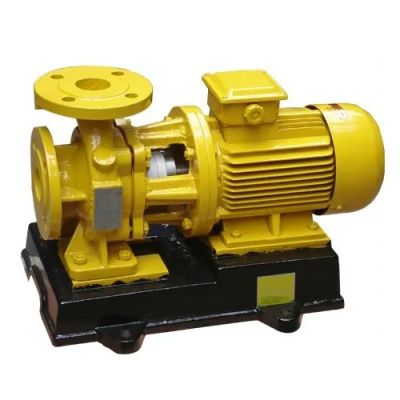
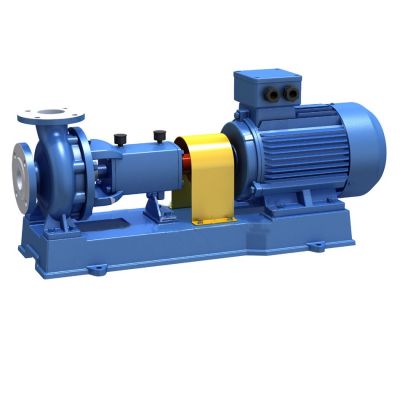
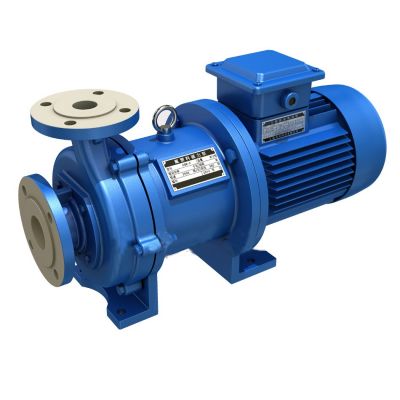
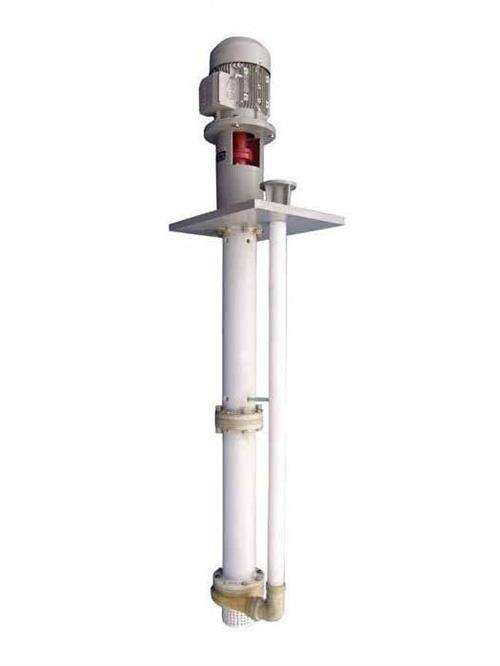
The GBW is a horizontal centrifugal pump built on ISW-type hydraulics for concentrated sulfuric acid.
| Item | GBW specification |
|---|---|
| Capacity | 4–550 m³/h |
| Head | 12.5–50 m |
| Size | DN25–DN250 |
| Speed | 2,900 rpm |
| Gray cast iron version (HT200/HT250) | 80–98% acid, 25–50 °C |
| WCB carbon steel version | 80–98% acid, 25–60 °C |
| Standard seal | External PTFE bellows single seal, no cooling water needed |
Where the concentration can fall below 80% or the temperature exceeds 60 °C, use a fluoroplastic-lined pump instead, as described in the next section. The full range is in our chemical process pumps category.
The IHF and CQB-F are lined with FEP (F46), a fluoroplastic that resists 98% sulfuric acid without being oxidized by it. Chemical resistance is not the whole story, though. Temperature, water and the extra weight of the acid still decide how long a lined pump lasts.
| IHF lined centrifugal pump | CQB-F lined magnetic drive pump | |
|---|---|---|
| Lining | FEP (F46) | FEP (F46) |
| Flow and head | 3–130 m³/h, 5–87 m | 1.8–100 m³/h, 8–32 m |
| Published liquid temperature | Up to 80 °C | Up to 80 °C |
| Shaft sealing | Mechanical seal: SiC/SiC faces, PTFE bellows, Hastelloy C-276 springs | No shaft seal |
| Best for | Steady duty and larger flows | Zero-leakage duty at small and medium flows |
| Main risk | Leakage at the mechanical seal | Dry running, cavitation and gas, which destroy the internal bearings |
Three conditions apply to both pumps:
- Temperature protects the lining bond, not just the plastic. FEP and the steel casing expand at very different rates, so high temperature and rapid heating or cooling can blister the lining or separate it from the steel. Do not run at the top of the range, and avoid thermal shock.
- Keep water out. Water or weak acid entering the pump dilutes the acid locally and releases heat, and that local hot spot can blister the lining.
- Size the motor for SG 1.84. Published motor ratings are for water, as the next section explains.
The CQB-F has two further requirements. Its internal bearings are lubricated and cooled only by the pumped acid, so a few minutes of dry running, cavitation or entrained gas can melt the bearings, overheat the containment shell and demagnetize the magnets. Concentrated acid is heavy and viscous, which makes cavitation more likely, so check NPSH with a clear margin and fit dry-running protection, such as motor power monitoring or a flow switch. The magnetic coupling must also be rated for the acid: a coupling sized for water can slip and lose its magnetism at SG 1.84, so both the coupling torque and the motor power have to be increased. Keep the liquid at or below 80 °C, because the risk of demagnetization rises with temperature. For more on sealless pumps, see how to select a magnetic drive pump.
Density does not change the head a centrifugal pump develops, but it raises the discharge pressure and the power in direct proportion. Sulfuric acid at 93% to 98% has a density of about 1.83 to 1.84 kg/L, and acid at 78% to 80% about 1.70 to 1.73. Size the motor for the strongest acid the pump will see. For how head and pressure relate, see what pump head means.
Catalogue tables, including the GBW table, are rated on water (SG 1.0) unless they say otherwise. Take the GBW65-160 as an example: 25 m³/h at 32 m, listed with a 5.5 kW motor. Assuming a pump efficiency of 60%:
Shaft power = ρ × g × Q × H ÷ η
Water: 1,000 × 9.81 × (25 ÷ 3,600) × 32 ÷ 0.60 ≈ 3.6 kW
98% acid: 1,840 × 9.81 × (25 ÷ 3,600) × 32 ÷ 0.60 ≈ 6.7 kW
The 5.5 kW motor is fine for water and overloaded on 98% acid. With a service margin added, the next standard size is 7.5 kW, or 11 kW if your standard applies a 15% margin. Concentrated acid is also about 25 times as viscous as water at 20 °C, which lowers efficiency a little further. Before ordering any concentrated sulfuric acid pump, ask the supplier to confirm in writing that the motor has been sized for SG 1.84.
The GBW's standard seal is a WB2-type external PTFE bellows single seal. It sits outside the acid and needs no cooling water. Seal configurations vary between manufacturers, so specify these items in the contract:
| Seal part | Specify | Avoid |
|---|---|---|
| Seal faces | Silicon carbide against silicon carbide (SiC/SiC) | Ceramic against graphite: concentrated acid slowly oxidizes graphite |
| Alternative faces | 99% alumina ceramic against SiC: cheaper, less resistant to thermal shock | — |
| Secondary seals | PTFE | — |
| Springs and small metal parts | Hastelloy C-276 | 304 stainless steel: acid mist corrodes it and the seal sticks |
The same seal configuration applies to the IHF lined pump.
- Never below 80% concentration. The protective film dissolves and corrosion accelerates. Keep cast iron and carbon steel out of the 65–80% range entirely.
- No oleum in cast iron. Free sulfur trioxide reacts with the silicon in cast iron and makes it brittle and cracked. Carbon steel tolerates oleum above 102% only for short periods.
- No high velocity or gas scouring. Fast flow and bubbles wear the film away.
- Stay within the temperature limit: 50 °C for gray cast iron, 60 °C for WCB carbon steel.
- No water left in the pump. Diluted acid attacks the iron and releases heat.
- Acid concentration: minimum, normal and maximum, including startup, cleaning and upset conditions.
- Liquid temperature: normal and maximum.
- Flow rate and total head, with the suction conditions and NPSH available.
- Impurities and solids, and whether water can enter the system.
- Operating pattern: continuous, batch, or intermittent transfer.
- Installation: horizontal pump with flooded suction, or transfer from a tank or sump.
- Motor standard, voltage and frequency, and a request to confirm the motor for SG 1.84.
- Seal configuration: SiC/SiC faces, PTFE secondary seals and Hastelloy C-276 springs.
- For a magnetic drive pump: a magnetic coupling rated for SG 1.84, and dry-running protection.
Need a pump for sulfuric acid? Send these details to SHINJO and we will recommend a model and material for your concentration and temperature.
For 80% to 98% acid, gray cast iron is suitable up to 50 °C and WCB carbon steel up to 60 °C, because the acid forms a protective iron sulfate film on them. Above those temperatures, or where the concentration can fall below 80%, a fluoroplastic-lined pump is the safer choice.
No. Below 80% the protective film dissolves, and the range from 65% to 80% is the most aggressive for iron. Use a fluoroplastic-lined pump for that range.
Only within narrow concentration and temperature windows. Common grades such as 316 corrode badly in the middle of the concentration range, so stainless steel is not a default choice for sulfuric acid pumps.
Yes, chemically. FEP and PTFE linings resist 98% sulfuric acid. The limits are temperature, published as 80 °C for the IHF and CQB-F to protect the bond between lining and steel; keeping water out of the pump; and sizing the motor for SG 1.84.
No. Its internal bearings are lubricated and cooled by the acid itself, so dry running, cavitation or gas bubbles can destroy the bearings and demagnetize the coupling within minutes. Fit dry-running protection and make sure the coupling is rated for SG 1.84.
No. The head stays the same, but the discharge pressure and the power rise in proportion to density, so 98% acid needs about 1.84 times the shaft power of water.
